
Helium Leak Detection: How MPF Products Verifies Hermetic Seals
MPF Products helium leak tests its vacuum components and assemblies to a leak rate of less than 1 x 10⁻⁹ atm cc/sec. In an ultra-high vacuum (UHV) system, a microscopic leak at a braze joint, weld, or ceramic-to-metal seal can limit base pressure, admit contaminants, and compromise the process the system was built to run.
Helium mass spectrometer leak detection is the industry-standard method for locating and quantifying leaks of this size. This page explains why helium is used as the tracer gas, how a helium leak detector works, the two principal test methods, and how MPF Products applies them in production.
Why Helium Is the Preferred Tracer Gas
Helium leak testing works by introducing helium at a potential leak path and detecting any helium that passes through it. Several properties make helium well suited to this role:
- Small, light, monatomic atoms. Helium is the second-lightest element and exists as single atoms. Its small atomic size and high diffusivity make it especially effective at revealing very small leak paths.
- Low natural background. Helium makes up only about 5 ppm of ambient air, so a rise in helium signal can be attributed to a leak with confidence. Helium can accumulate near active leak-test stations, so modern leak detectors include background suppression to keep readings reliable.
- Unambiguous detection. At mass 4, helium is easily separated from other gases by a mass spectrometer.
- Safe and clean. Helium is chemically inert, non-toxic, and non-flammable, and leaves no residue on UHV surfaces.
How a Helium Mass Spectrometer Leak Detector Works
A helium leak detector is a compact, self-contained vacuum system built around a mass spectrometer tuned to detect helium. Its operation follows a consistent sequence:
- Evacuation. The leak detector’s roughing and turbomolecular pumps evacuate the test port and the part connected to it.
- Ionization. Gas drawn from the part enters the spectrometer, where a heated filament ionizes it by electron bombardment.
- Mass separation. The ions are accelerated through a magnetic field. Ions of different mass follow paths of different radius, and only helium ions follow the path that reaches the detector.
- Measurement. The resulting ion current is proportional to the helium partial pressure. The instrument converts this signal into a calibrated leak rate and displays it directly.
The spectrometer only operates under high vacuum, while the part under test starts at atmospheric pressure. Many modern leak detectors resolve this with a counterflow design. Gas from the part enters the turbomolecular pump partway along its stages rather than passing straight into the spectrometer. The pump strongly compresses heavier gases and holds them back, but light helium atoms diffuse backward against the pumping direction to reach the spectrometer. The result is fast testing at relatively high part pressures, with the spectrometer kept clean and protected.
Test Methods: Vacuum Mode and Sniffer Mode
Helium leak detectors are used in two principal configurations. For UHV components, vacuum mode is the more sensitive and more relevant method.
| Vacuum mode (outside-in) | Sniffer mode (inside-out) | |
|---|---|---|
| Part condition | Evacuated by the leak detector | Pressurized with helium |
| Where helium is applied | Sprayed on the exterior of the part | Inside the part |
| How leaks are found | Helium drawn through a leak reaches the spectrometer | A probe samples the air around the part |
| Relative sensitivity | Highest; detects leaks well below UHV acceptance limits | Several orders of magnitude lower, because surrounding air dilutes the sampled helium |
| Typical use | Vacuum components, feedthroughs, welded and brazed assemblies | Pressurized systems, gas lines, components that cannot be evacuated |
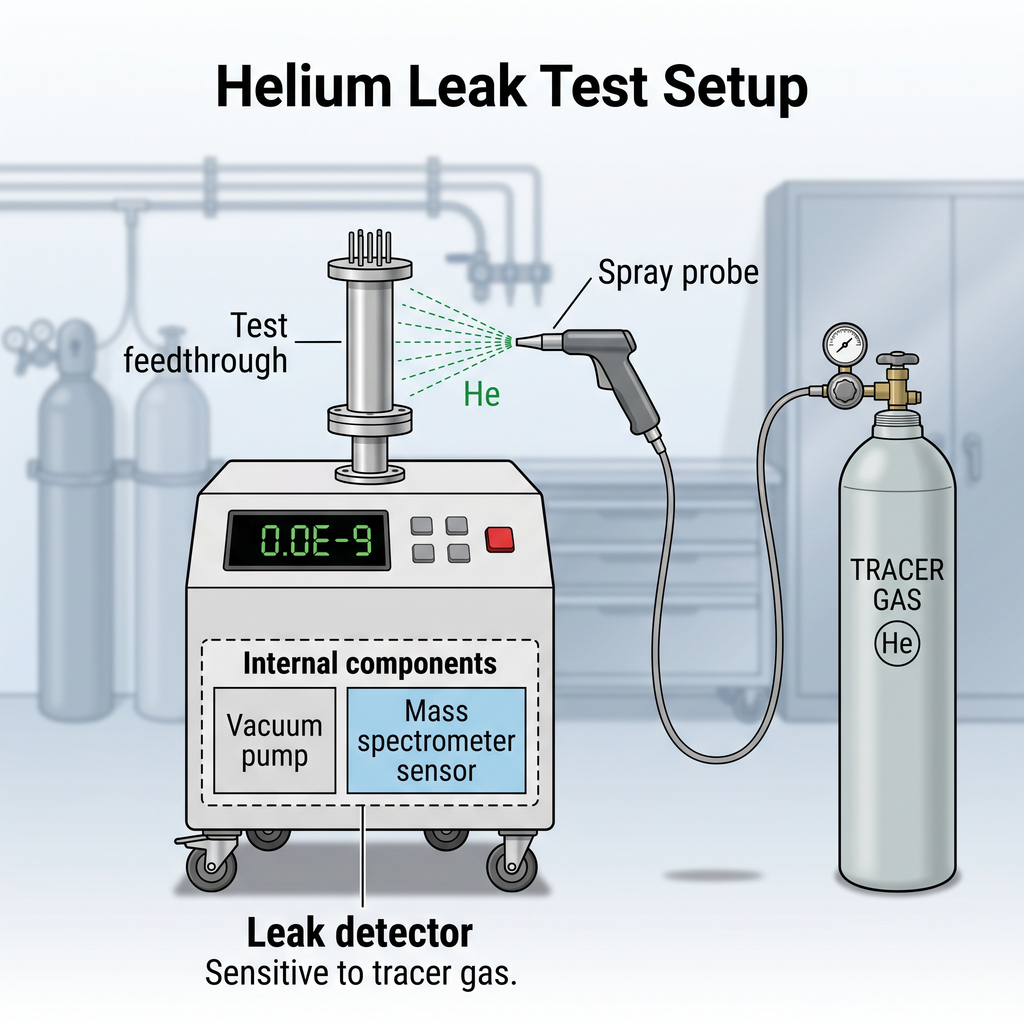
In vacuum mode, the operator typically sprays a controlled stream of helium at individual joints and seams while monitoring the leak rate signal. A rise in signal identifies the location of a leak. Alternatively, the entire part can be enclosed in a helium-filled hood or chamber to measure its total, or integral, leak rate. Integral testing confirms whether a part meets an overall specification, but it does not locate individual leaks.
Understanding Leak Rates
MPF Products’ standard acceptance criterion is a helium leak rate of less than 1 x 10⁻⁹ atm cc/sec (approximately 7.6 x 10⁻¹⁰ Torr·L/sec). Leak rate expresses the amount of gas passing through a leak per second, stated as the equivalent volume the gas would occupy at atmospheric pressure.
At 1 x 10⁻⁹ atm cc/sec, it would take more than 30 years for a single cubic centimeter of helium to pass through the seal. For applications that require tighter verification, MPF Products can test to 1 x 10⁻¹⁰ atm cc/sec and below on request.
Leak Testing at MPF Products
MPF Products performs helium leak testing in vacuum mode, the more sensitive of the two methods, using helium mass spectrometer leak detectors capable of detecting leaks well below our acceptance limits.
An instrument’s detection limit and a part’s acceptance limit are different numbers. The detection limit is the smallest leak the instrument can sense under specified conditions. The acceptance limit is the largest leak rate a part may have and still pass. Because the detection limit of our test equipment sits far below our standard acceptance limit, the equipment has ample sensitivity to judge each part against the specification.
Our test procedure for brazed and welded components and assemblies:
- The part is connected to the leak detector’s test port and evacuated.
- Once the leak detector reaches its measurement range, helium is sprayed at each braze joint, weld, and seal.
- Leak rate readings are monitored throughout testing. Any indication of a leak at or above the acceptance limit is investigated, and the affected area is reworked and retested as necessary.
- Parts are tested at multiple stages of manufacture, so a leak is caught before it can be built into a larger assembly.
Specify a Leak-Tight Assembly
Every hermetic component MPF Products ships is helium leak tested before it leaves our facility. If your application requires a specific leak rate, test method, or test documentation, contact our engineering team to discuss your requirements.